Watertight 3D Printed Parts: Enclosures, Tanks and Fluid Channels
Why printed walls leak and how to stop it: FDM wall design, SLA, sealing coatings, gaskets and O-ring glands, what an IP rating means, and how to leak-test.
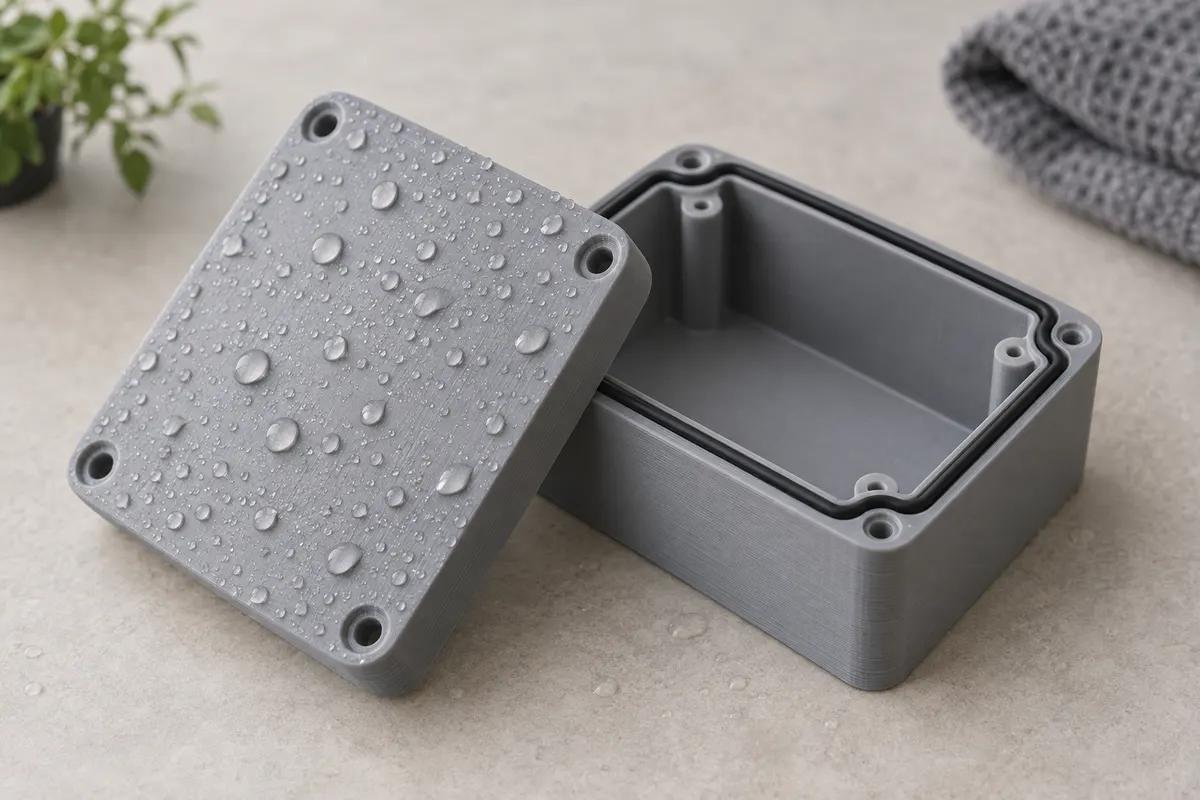
The Short Answer
A printed part can keep water out or hold liquid in, but only by design and by test. FDM walls leak through pores between extruded lines, so a liquid-holding FDM part needs thick, fully fused walls with few sharp edges or abrupt transitions; SLA builds a continuous cured wall but still needs a leak test. Water usually gets into an enclosure at its joints, cable entries and vents, so the seal design matters more than the walls. No printed design has an IP rating until the enclosure has been tested to IEC 60529.
Two Different Jobs
Keeping water out of an enclosure and holding liquid inside a tank, channel or manifold fail in different places. An enclosure usually leaks at its interfaces: the lid joint, the cable entries and anything that lets it breathe. A vessel has to stop liquid at the wall itself, often under pressure, so the structure of the wall matters as much as its joints. Anything that holds pressure or hazardous liquid, or could hurt people or property if it leaks, needs your own engineering and testing. This guide gives design starting points, not ratings.
Why FDM Walls Leak
- Pores between beads. A University of Washington review of 3D-printed microfluidics (Au, Huynh, Horowitz and Folch, 2016) notes that walls built from extruded filaments are prone to pores because adjacent layers are not well fused.
- Seams that line up. Gordeev, Galushko and Ananikov (PLOS ONE, 2018) found that when the start-and-stop seams of a wall's perimeters coincide, a pore runs straight through. Walls of about 0.5 mm, made only of perimeters, were often impossible to seal at any setting they tried.
- Under-extrusion and narrow lines. Irimia, Ermolai and Nagîț (Gheorghe Asachi Technical University of Iași, 2025) saw under-extruded cylinders leak along the vertical seam and where the bottom met the side wall, and gaps open between contour lines when the lines were narrow.
- Shape. Gordeev et al. found edges and vertices more prone to pores than other areas, and conical or curved walls, whose layers are offset from one another, more vulnerable than flat and cylindrical walls whose layers sit directly on one another.
- Transitions. In a University of Texas at El Paso study of sealed FDM pressure caps (Mireles et al., 2011), most failures were where geometry changed, such as a flat surface turning into a round one.
Designing an FDM Part to Hold Liquid
- Make wetted walls thick, with several perimeters. Thicker walls sealed better in both studies above: Irimia et al. found wider lines sealed better than narrow ones, and Gordeev et al. found walls with room for fused material between the perimeters better than walls made of perimeters alone. Irimia et al. also cite earlier work on PLA in which four walls and thin layers gave compact structures that resisted liquid penetration.
- Orient wetted walls to stand vertical in the build where possible, so each layer sits directly on the one below, and avoid sloped or conical wetted walls.
- Avoid sharp edges, vertices and abrupt changes of shape on wetted surfaces; blend them with fillets.
- Choose the material for the liquid and the environment. In Gordeev et al., PLA, ABS, PETG, PP, nylon and carbon-filled nylon all sealed once the print settings suited them, so sealing alone does not decide the material. PETG is a common general-purpose choice, ASA suits sun exposure and polypropylene suits many chemicals. Nylon absorbs water and changes size; see nylon dimensions and moisture.
- Tell the team through the contact page that the part must hold liquid. The free printability review checks walls, tolerances, orientation and material choice.
SLA: A Continuous Wall, Still Tested
SLA cures each layer from liquid resin instead of laying down separate beads. Au et al. describe stereolithography as one of the only 3D-printing techniques that allow routine fabrication of closed microfluidic channels. The same review gives two cautions: channels are emptied by draining uncured resin, which takes design attention and handling, and some resins resist water but not organic solvents. For SLA parts, give internal channels openings large enough to drain and rinse, and check the resin against your fluid. How to choose an SLA resin is a starting point, and Glass-Filled Rigid Resin is the stiff resin our catalog lists for fluid manifolds. SLA's general tolerance of about ±0.1 mm also matters for O-ring grooves, below.
Sealing Coatings
A coating can close pores that design and print settings leave behind. Mireles et al. brushed or vacuum-infiltrated eleven sealants into FDM pressure caps and tested them under air pressure, under water. The best sealant let the caps hold pressure without bubbling, and several hardware-store polyurethanes and sealers also did well. Coatings have costs: the best sealant changed dimensions by an average of 0.231 mm when brushed and 0.104 mm when infiltrated, and sealant pooled at corners, edges and crevices as it cured. Sealing coatings are not among the finishes we offer, so if you plan one, allow for its thickness, keep it off sealing faces and threads, and test the coated part. Vapor smoothing, which we offer on ABS and ASA, melts the surface, but the same paper notes that its effect on sealing had yet to be investigated, so treat it as a surface finish unless your own test shows more.
Gaskets and O-Ring Glands
Water enters at the joints, so the joint is a seal design problem. A purchased O-ring in a printed groove is the most predictable option, because ring makers publish gland dimensions. Apple Rubber's seal design guide gives the rules:
- The ring must be squeezed: the gland depth is less than the ring's cross-section. Apple suggests a squeeze of roughly 10–40% for static seals.
- Keep no less than 75% of the cross-section inside the groove so the ring cannot roll out, and keep the ring's volume at or below 90% of the smallest gland void.
- A face seal on a rectangular lid can use a standard round O-ring if the groove's inside corner radius is at least three times the ring's cross-section, with the ring's centerline length equal to the groove's.
- Sealing faces need a smooth finish. Apple's static gland drawings call for 32 RMS on sealing surfaces for liquids and 16 for vacuum and gases. A printed face carries layer steps, and Buj-Corral et al. (Materials, 2019) tie that stair-stepping roughness to the face's angle to the layers. Put the sealing face parallel to the layers where you can, or plan to finish it.
Check the Groove Against Printed Tolerance
Apple Rubber's static table puts the axial gland depth for a ring of 0.139 in (3.53 mm) cross-section at 0.100 to 0.108 in (2.54 to 2.74 mm), a band only about 0.2 mm wide. FDM's general ±0.2 mm spans twice that band, and SLA's ±0.1 mm spans all of it, so a printed groove can land outside the band. Measure the groove depth on a first print and adjust the CAD, or choose a larger cross-section, whose band is wider. For how tolerances add up across a joint, see snap fits, press fits and clearances.
Keep the Lid Compressed
- Amorim Cork Solutions, a gasket material maker, notes that a gasket is compressed most where each fastener pulls, and that bowing of the cover depends on fastener spacing and on the cover's thickness and stiffness. A printed lid is far less stiff than a metal one, so add ribs, a thicker flange or more screws rather than relying on wide screw spacing.
- Put the screws in threaded inserts so the lid can be opened and closed again; see threaded inserts in 3D printed parts.
- A printed TPU 85A gasket can follow any outline and can be ordered with the box. It is still an elastomer seal, and Apple Rubber warns that over time an elastomer takes a compression set that can end in seal failure. Test a printed gasket over time, and use a catalog O-ring or cord where the groove allows. See TPU flexible printing.
Cable Entries, Vents and Condensation
- Use a purchased cable gland or sealed connector at every cable entry.
- Let a sealed box breathe through a membrane vent. W. L. Gore explains that rapid changes in temperature, air pressure or altitude create pressure differences that stress seals repeatedly until they fail, after which further pressure swings can draw liquids into the housing; a protective vent equalizes pressure while blocking water and dust.
- Plan for condensation separately. IEC 60529 lists moisture produced by condensation among the influences it leaves to product standards, so an IP code says nothing about it.
- Cooling vents and sealing conflict. The heat side is covered in the electronics enclosure checklist.
What an IP Rating Is
IEC 60529 classifies the degrees of protection provided by enclosures for electrical equipment: against access to hazardous parts and against solid foreign objects (the first numeral), and against harmful ingress of water (the second numeral). It also sets the tests that verify each degree, and it applies only to enclosures whose materials and workmanship maintain the claimed protection in normal use. So an IP code belongs to a tested enclosure, not to a material or a design, and a printed enclosure built to seal is the test article for that qualification. The water numerals most often asked about are tested like this:
| Second numeral | Test named in IEC 60529 |
|---|---|
| 5 | Water jets from a 6.3 mm nozzle |
| 6 | Water jets from a 12.5 mm nozzle |
| 7 | Temporary immersion between 0.15 m and 1 m |
| 8 | Continuous immersion, on terms subject to agreement |
How to Test a Printed Seal
- Bubble test for vessels and channels. ASTM E515 covers locating leaks by bubble emission, either by immersing the part or by applying a liquid film to it. It locates leaks on a go/no-go basis and does not measure a leak rate. Gordeev et al. and Mireles et al. both used the immersion form, pressurizing the part with air under water and watching for bubbles.
- Raise pressure slowly and stand behind a shield. Mireles et al. raised pressure gradually and warn that voids in FDM parts can let a pressurized part fail catastrophically.
- Confirm later. Mireles et al. repeated each passing test the next day to make sure the seal still held.
- Dunk or spray test for enclosures. Put dry paper inside, close the box exactly as it will be used, expose it to water the way the product will meet it, then open it and look.
- Cycle it. Temperature and pressure swings stress seals, so repeat the test after the box has been heated and cooled.
- For a rating, have the enclosure tested to IEC 60529 by a test lab.
Watertight Design Checklist
| Check | Why |
|---|---|
| Wetted FDM walls thick and vertical in the build | Thin and sloped FDM walls leak most |
| No sharp edges or abrupt transitions on wetted walls | Leaks cluster at edges and transitions |
| Process chosen for the job | SLA for closed channels; FDM with thick, fused walls |
| Material suits the liquid and environment | Sealing alone does not pick the material |
| Purchased O-ring in a gland from the maker's table | Squeeze, fill and finish are then defined |
| Groove depth checked against the gland band | Printed tolerance can exceed the band |
| Lid stiff enough between fasteners | Compression is highest at each screw |
| Cable glands and a membrane vent | Interfaces and pressure swings let water in |
| Coating thickness and masking planned | Coatings change dimensions and pool |
| Tested, then tested again after cycling | Seals can fail over cycles, not on day one |
| IP code only from an IEC 60529 test | A design or a material is not rated |
Ordering Sealed Parts
Upload the housing, lid and gasket, or the vessel, on the quote page. A TPU gasket and an FDM box can sit in the same order as an SLA part, each priced by its own process and material. Note that the part must seal or hold liquid, and when you enter your contact details, tick Engineering / DFM review for the free printability review of walls, tolerances, orientation and material choice. The review checks printability; sealing performance is proven by your test. Quantity pricing tiers are applied automatically, from test units to production. We do not sell printed parts for food or drinking-water contact.
Frequently asked questions
Are FDM 3D prints waterproof?
Is SLA better than FDM for parts that hold liquid?
Can you make my enclosure IP67?
Should I use a printed TPU gasket or a standard O-ring?
Can a printed tank hold drinking water?
Sources
- Au, Huynh, Horowitz and Folch, Angewandte Chemie (2016): 3D-Printed Microfluidics
- Gordeev, Galushko and Ananikov, PLOS ONE (2018): Improvement of quality of 3D printed objects by elimination of microscopic structural defects in fused deposition modeling
- Irimia, Ermolai and Nagîț, Bulletin of the Polytechnic Institute of Iași (2025): Study on the Tightness of Parts Manufactured by FDM
- Mireles et al., University of Texas at El Paso, Solid Freeform Fabrication Symposium (2011): Analysis of Sealing Methods for FDM-fabricated Parts
- Buj-Corral, Domínguez-Fernández and Durán-Llucià, Materials (2019): Influence of Print Orientation on Surface Roughness in FDM Processes
- Apple Rubber: Seal Design Guide, Section 3, O-Ring Basics
- Apple Rubber: Seal Design Guide, Section 4, Seal Types and Gland Design Tables
- Apple Rubber: Face Seal Applications (Non-Round)
- Amorim Cork Solutions: Gasket Design Guidelines
- W. L. Gore and Associates: ePTFE Membranes Relieve Pressure to Prevent Damage to Outdoor Electronic Housings
- IEC 60529: Degrees of protection provided by enclosures (IP Code), preview via VDE Verlag
- ASTM: E515-11(2022) Standard Practice for Leaks Using Bubble Emission Techniques
Upload your sealed part for review
Send the housing, lid and gasket, or the vessel, with a note on the liquid and how it must seal. Each part is priced by its own process and material.
Upload your parts